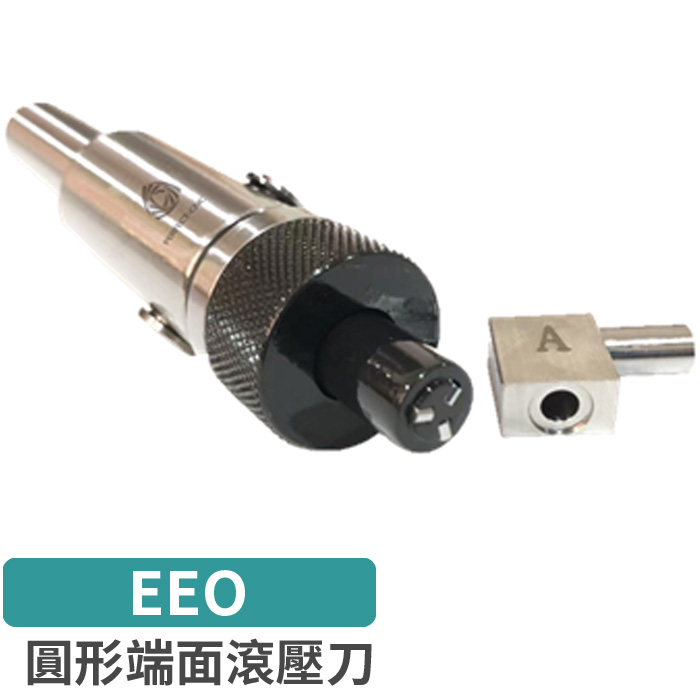
EEO Flat Surface Roller Burnishing Tool
Characteristic
Model : EEO
The EEO series flat surface roller burnishing tools are designed to enhance the surface finish of metal workpieces with high efficiency. These tools can be installed on conventional milling machines, lathes, boring machines, and CNC machining centers. Through rotation of either the tool or the workpiece, the finished surface can reach a roughness as low as Ra ≤ 0.2μm — no special equipment required.Flat Surface Roller Burnishing Tool
Key Features:
Suitable for roller burnishing of metal materials with hardness below HRC40.
JH-PD is ideal for circular flat surfaces with a minimum workpiece diameter of Ø5mm.
Achieves exceptional surface finish, with roughness ranging from Ra 0.05 to 0.2μm.
Reduces polishing time by 5 to 10 times, significantly improving work efficiency.
Can be used in either tool-rotation or workpiece-rotation modes.
Custumized design available upon request; easy to install and operate.
Main Components:
Screw Cap, Retainer, Rollers, Shaft, Housing, Straight Shank / Weldon Shank.
Recommended Operating Parameters:
| Model | Spindle Speed (r/min) | Indentation Depth (mm) | Feed Rate (mm/rev) |
|---|---|---|---|
| EEO | 200–800 | 0.02–0.05 | 0.1–0.3 |
Applicable Machines:
Conventional milling machines, lathes, boring machines, CNC machining centers, etc.
Maintenance & Operation Notes
1. Routine Maintenance:
Regular cleaning and inspection can extend tool lifespan and prevent damage due to wear or foreign particles.
Replace rollers and retainer as needed. Disassemble by removing the cap to access the components.
2. Shaft Replacement:
Unscrew the cap to remove rollers and retainer, then extract the shaft. Clean and lubricate thoroughly before reassembly.
Apply rust-prevention after cleaning.
3. Coolant Recommendation:
| Material | Coolant Ratio (Oil:Water) |
|---|---|
| Steel | Machine Oil:Water = 3:7 |
| Aluminum | Machine Oil:Water = 3:7 |
| Brass | 32# Hydraulic Oil:Water = 3:7 |
| Cast Iron | Machine Oil:Water = 3:7 |
4. Usage Guidelines:
Select tool model based on workpiece material, hardness, and surface condition. Pre-testing is advised.
Ensure sufficient wall thickness of the workpiece. Thin parts should be reinforced.
Surface roughness before burnishing should be ≤ Ra3.2μm. Roller contact must be even and smooth.
Stop the machine immediately if abnormal vibration or noise occurs.
Tools not used as specified or modified are not covered under warranty.
Note:
Uniform surface texture before burnishing ensures optimal finishing results.
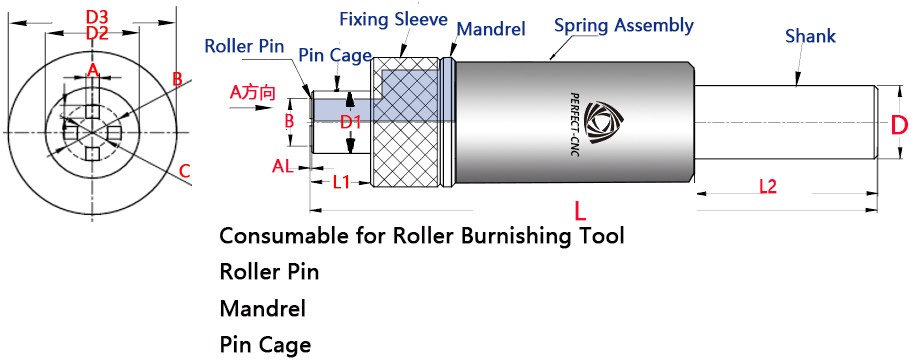
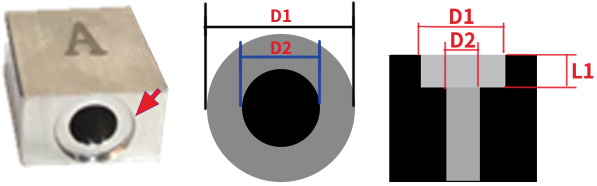
When placing the order, please provide the dimensions for D1, D2, and L1, as well as specify the type of shank you require.

 No. 21, Kaiyuan Rd., Dajia Dist., Taichung City 437024, Taiwan
 886-4-26865253
 886-4-26882279